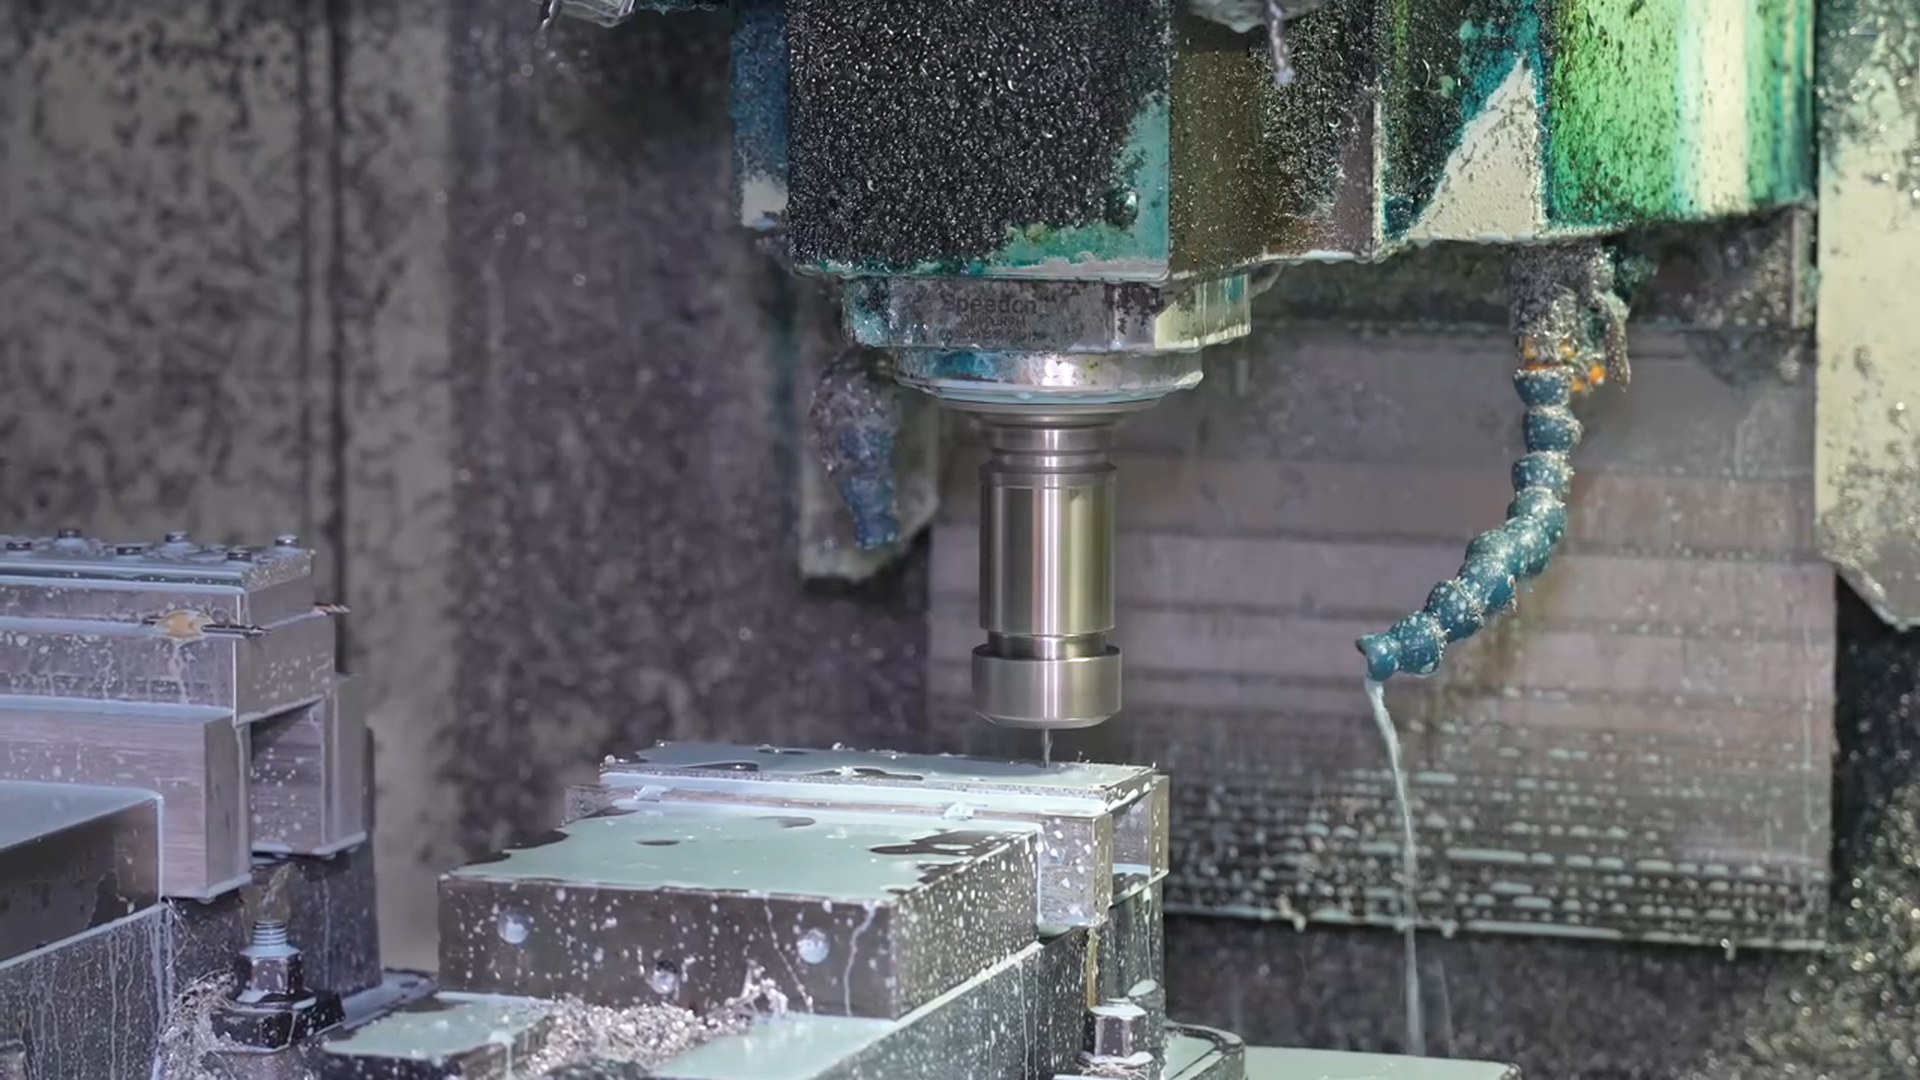
3-Axis CNC Milling Service
A direct option for flat profiles, pockets, drilled holes and accessible prismatic features. It is often the efficient choice when all critical geometry can be reached from standard setups.
Get a Quote
PRISMATIC FEATURES. DATUM-LED SETUPS.
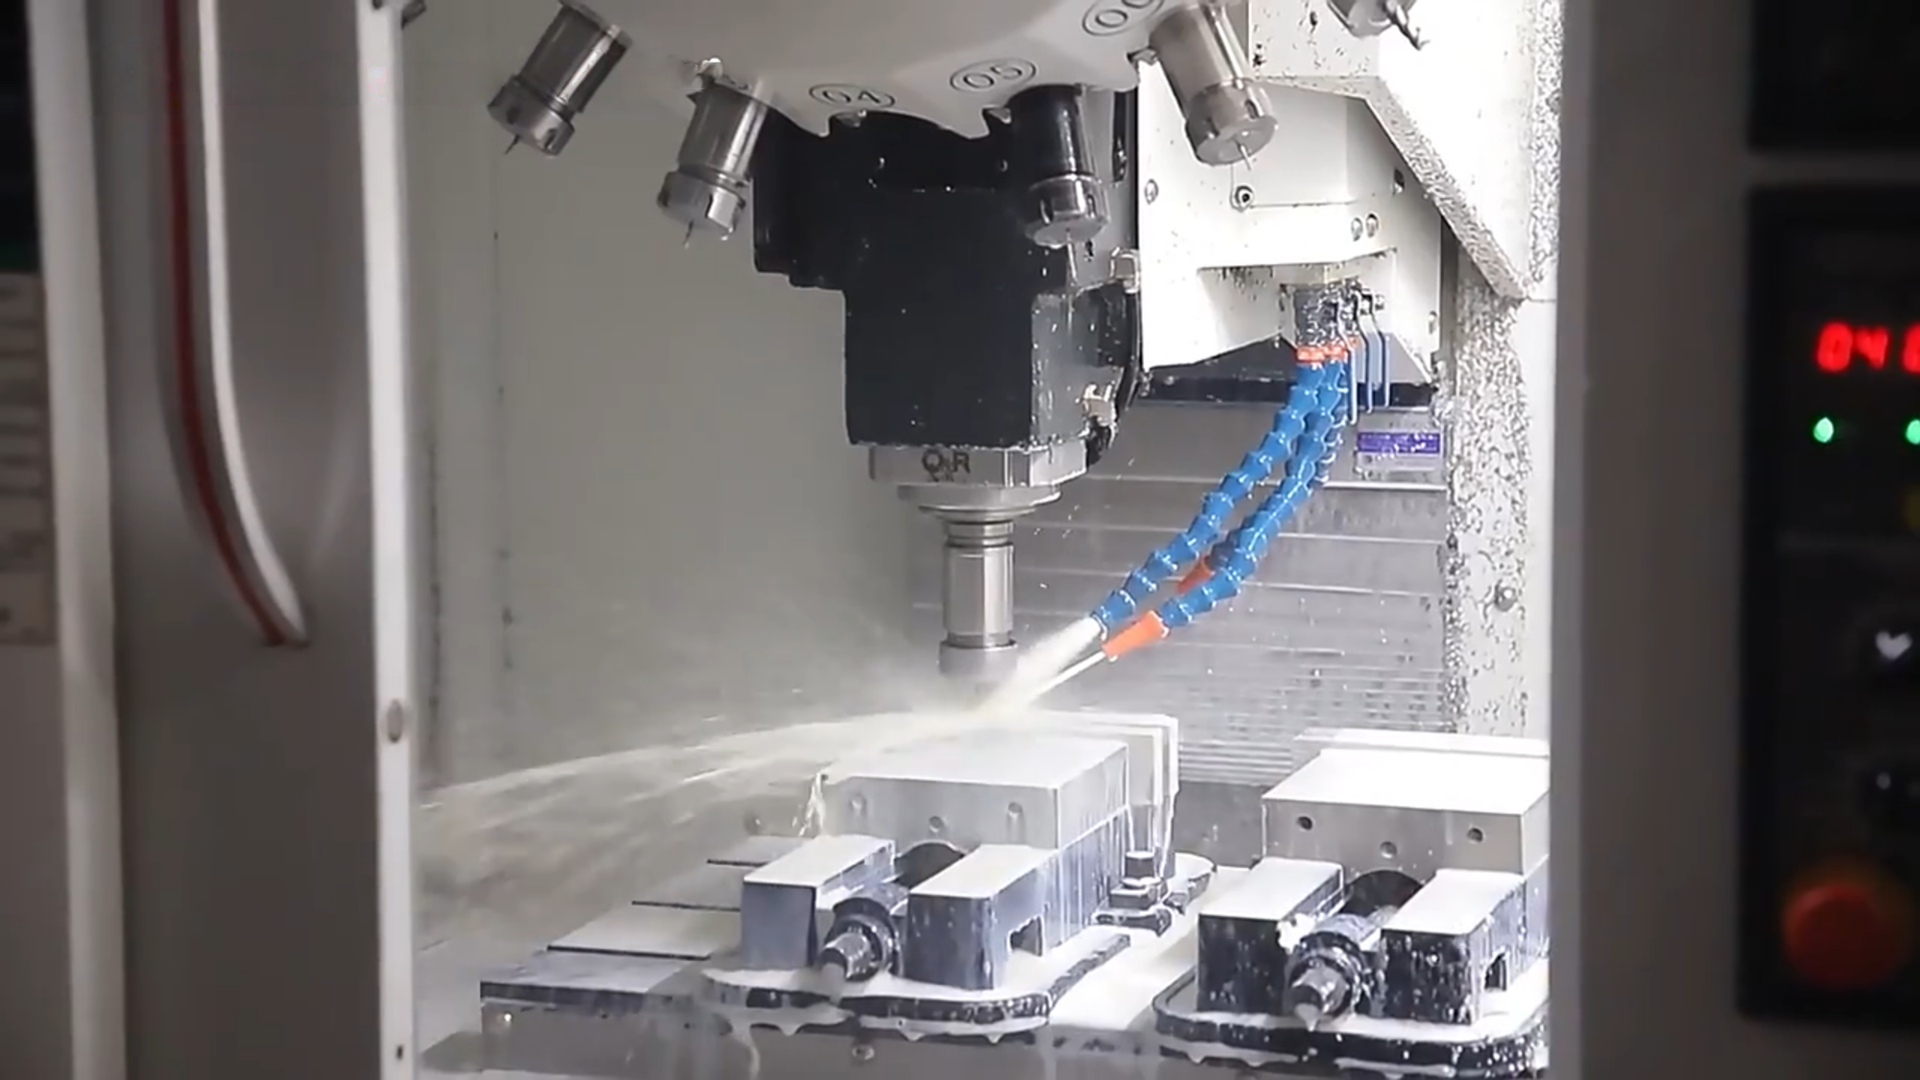
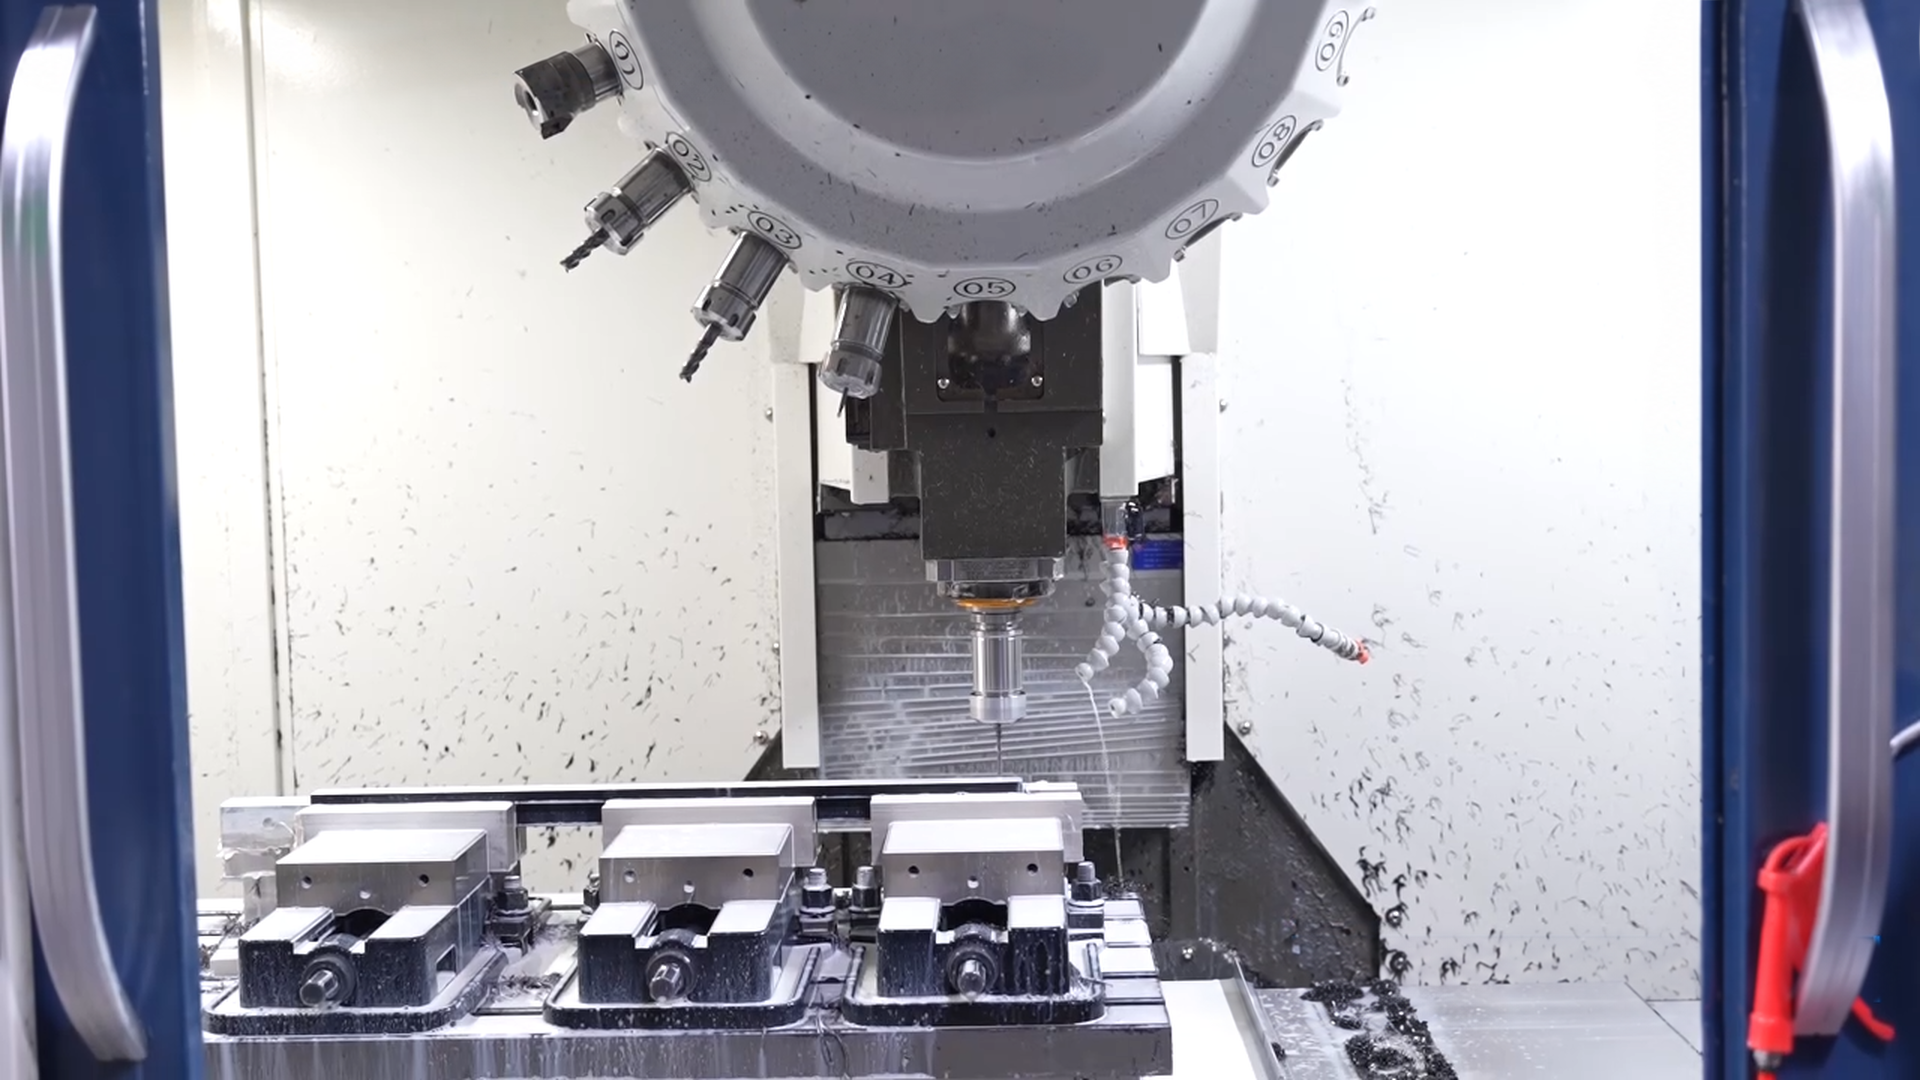
Our CNC milling service is suited to prismatic parts such as housings, brackets, plates, fixtures and heat sinks. We review the relationship between pockets, holes, flat surfaces, thin walls and datums before choosing the machining sequence. The stated maximum milling envelope is 1200 × 850 × 600 mm; final feasibility remains dependent on material, fixturing, wall stiffness and feature access.
 From Your Drawing
MANUFACTURING CAPABILITIES
A good milling plan begins with the locating faces and functional datums. It then selects the axis configuration and setup sequence that give the cutter access to pockets, holes and side features while protecting thin walls and critical relationships.
Our Full Capabilities →A direct option for flat profiles, pockets, drilled holes and accessible prismatic features. It is often the efficient choice when all critical geometry can be reached from standard setups.
Get a Quote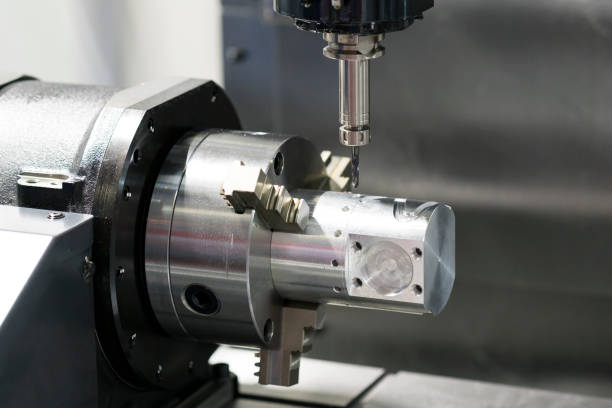
Rotary-axis positioning can expose features around a part with fewer re-clamps. It is considered when indexed side access improves alignment between holes, flats and other multi-face details.
Get a Quote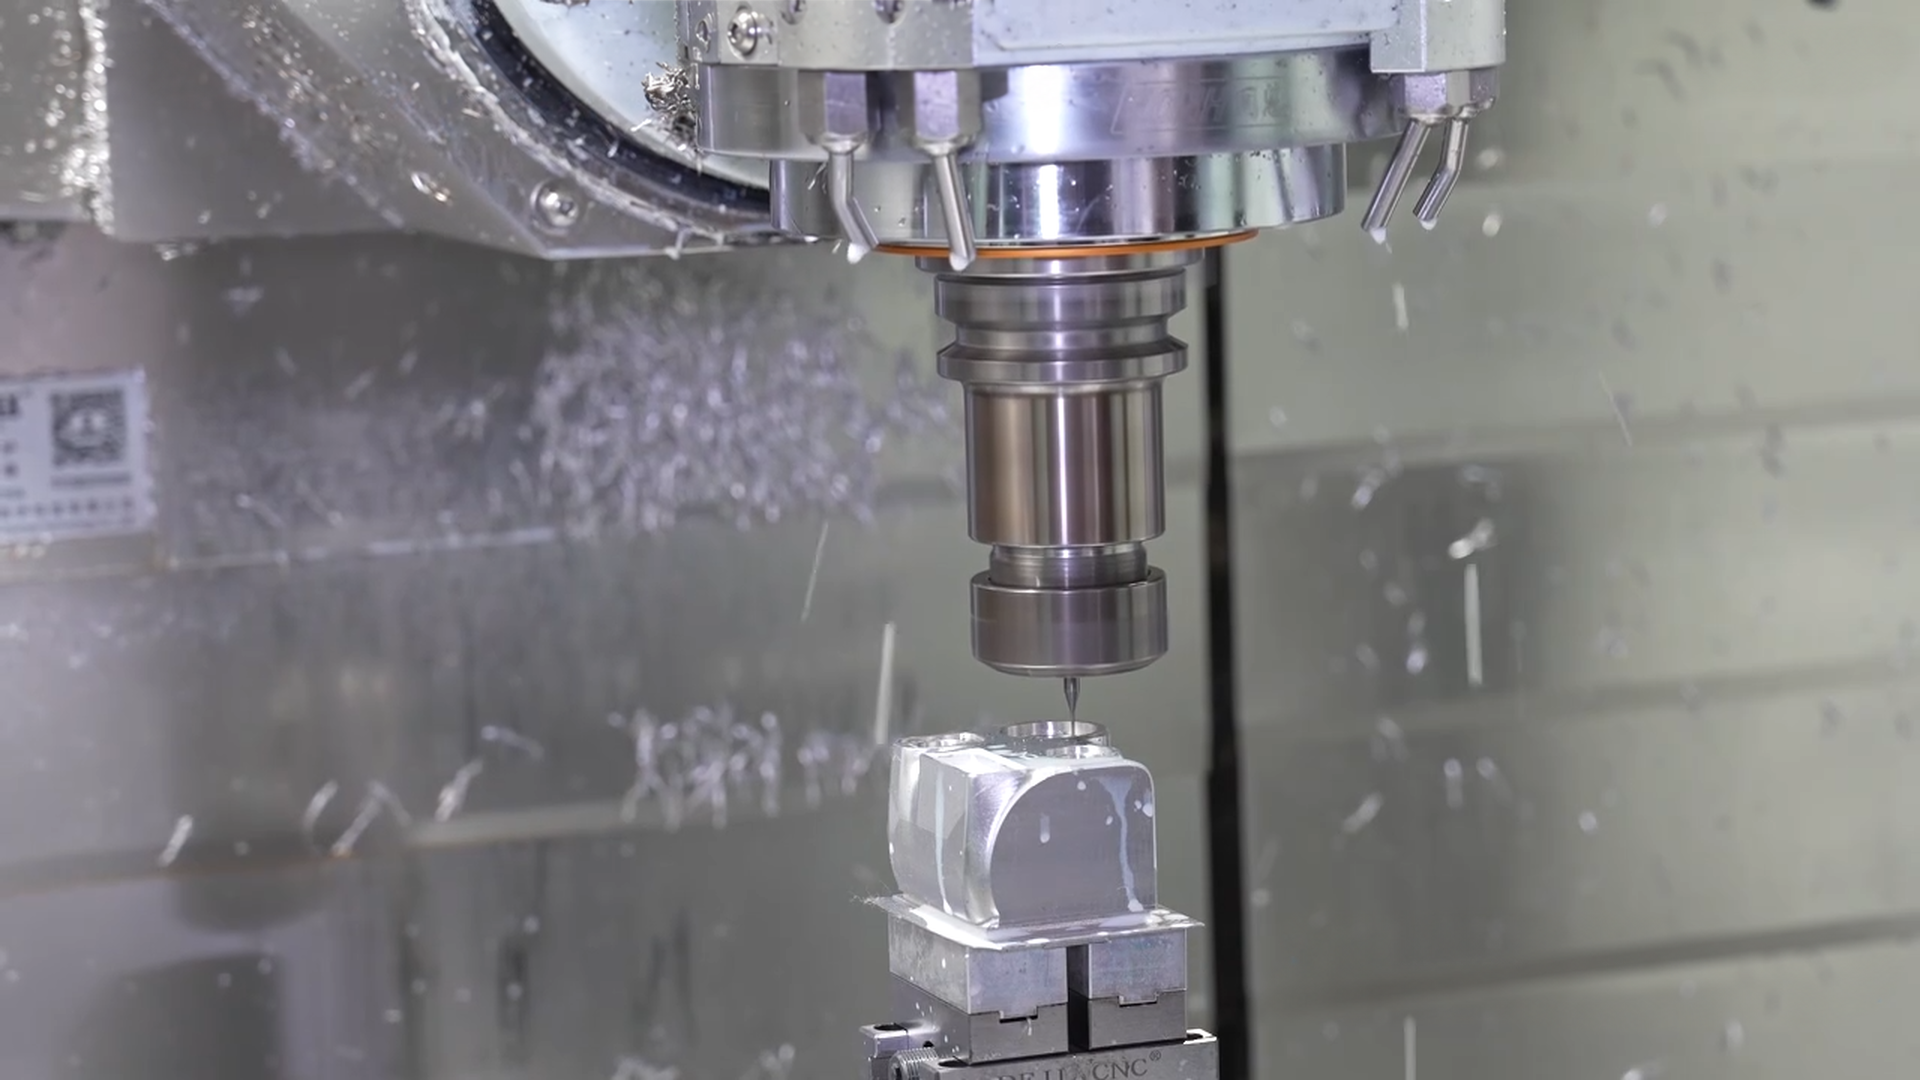
Used when compound angles, difficult access or multiple critical faces make an indexed or simultaneous multi-axis strategy more suitable. The process is selected from the drawing, not assumed for every complex part.
Get a QuoteMATERIAL OPTIONS
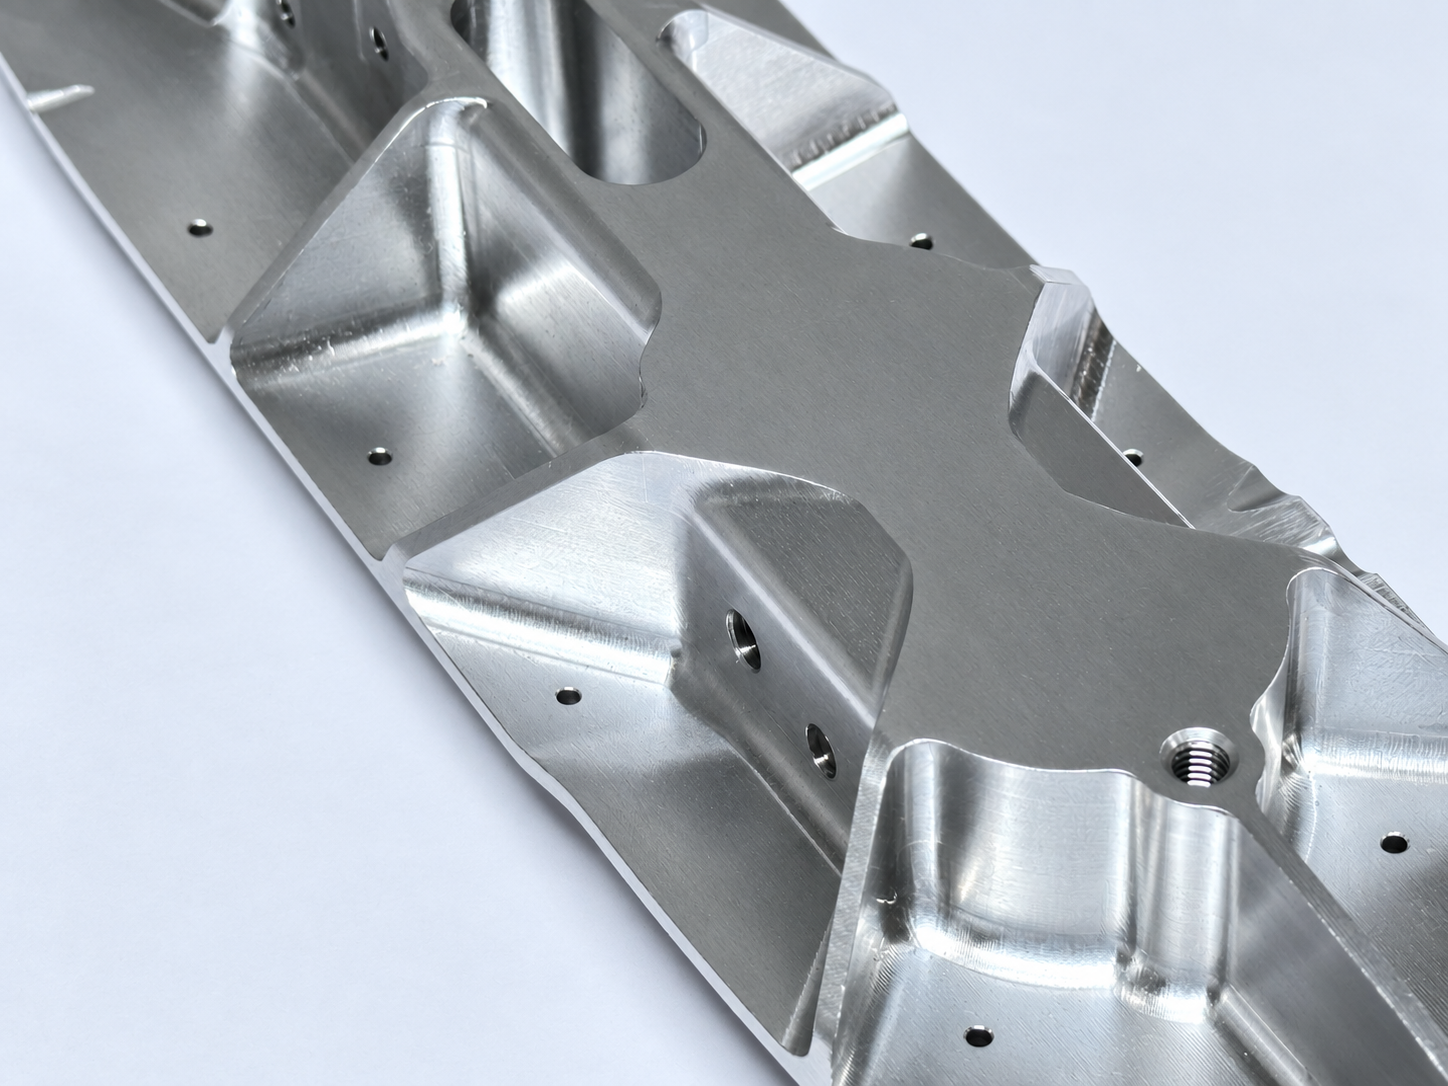
For milled parts, material rigidity, thin-wall behavior, pocket depth, thermal behavior, fixture strategy and finish requirements all affect the machining sequence and the features that need protection.
 Material guide
SELECTED MATERIAL
A practical choice where low mass, corrosion resistance and efficient machining are important.
SURFACE FINISHES
Identify flat mounting faces, critical holes, threads and surfaces that must remain as machined before selecting a cosmetic or protective finish. Specify any masking or downstream assembly requirement in the drawing.
A precise, cost-effective finish straight from the CNC process for functional features and tight tolerances.
View MoreImproves corrosion and wear resistance on aluminum, with clear, black and custom color options.
View MoreReduces surface roughness to create a smooth, refined appearance for visible precision components.
View MoreCreates a uniform matte texture and can reduce visible machining marks on suitable parts.
View MoreA durable, protective coating with a broad range of colors and textures.
View MoreAdds a protective or decorative metal layer for performance and appearance.
View MoreA dark conversion finish for steel parts requiring a low-reflective, corrosion-resistant surface.
View MoreBUILT FOR A WIDE RANGE OF INDUSTRIES
Suitable for housings, brackets, plates, fixtures, heat sinks and other prismatic parts that need controlled pockets, holes, flat faces or multi-face relationships. The relevant question is feature access and datum strategy, not industry label.
Explore All Applications →
Milled brackets, housings and prototype vehicle components
Complex lightweight structures, fixtures and equipment parts
Precision device housings, instruments and laboratory components
Milled RF housings, heat sinks and mounting hardware
Thermal plates, equipment brackets and power-system components
Milled housings, mounts and corrosion-conscious equipment parts
BUILT FOR DEMANDING PROJECTS
The drawing review focuses on the locating faces, accessible features and fixture approach that determine whether 3-, 4- or 5-axis access is appropriate.
Identify the locating faces and functional datums that control the part’s critical relationships.
Review pockets, holes, side features and multi-face details before selecting the axis configuration.
Thin walls, open pockets and material stiffness affect clamping and machining sequence.
Separate functional faces from cosmetic surfaces and identify areas that must remain as machined.
Call out critical holes, flatness-related relationships and documentation requirements in the drawing.
A CLEARER PATH TO YOUR PARTS
The milling plan is built around datums, feature access, wall condition and finish keep-out areas before any axis configuration is selected.
Provide 2D/3D drawings with material, quantity, datums, critical holes, wall conditions, tolerance and finish requirements.
Review datum strategy, tool access, pockets, thin walls, fixture approach and finish keep-out areas.
3-, 4- or 5-axis milling is selected for the required pockets, holes, faces, feature access and datum relationships—not simply by part size.
Drawing-defined checks for datum-related features, pockets, holes, flat faces and agreed documentation.
Production and shipment planning based on the agreed schedule, approved drawing, finish and shipping terms.
QUALITY ASSURANCE
Inspection is planned from the locating faces, functional datums and features that affect assembly. T-One applies 100% inspection against the drawing and agreed inspection requirements; dimensional, CMM, FAI and material documentation can be provided when specified.
Our Quality Process →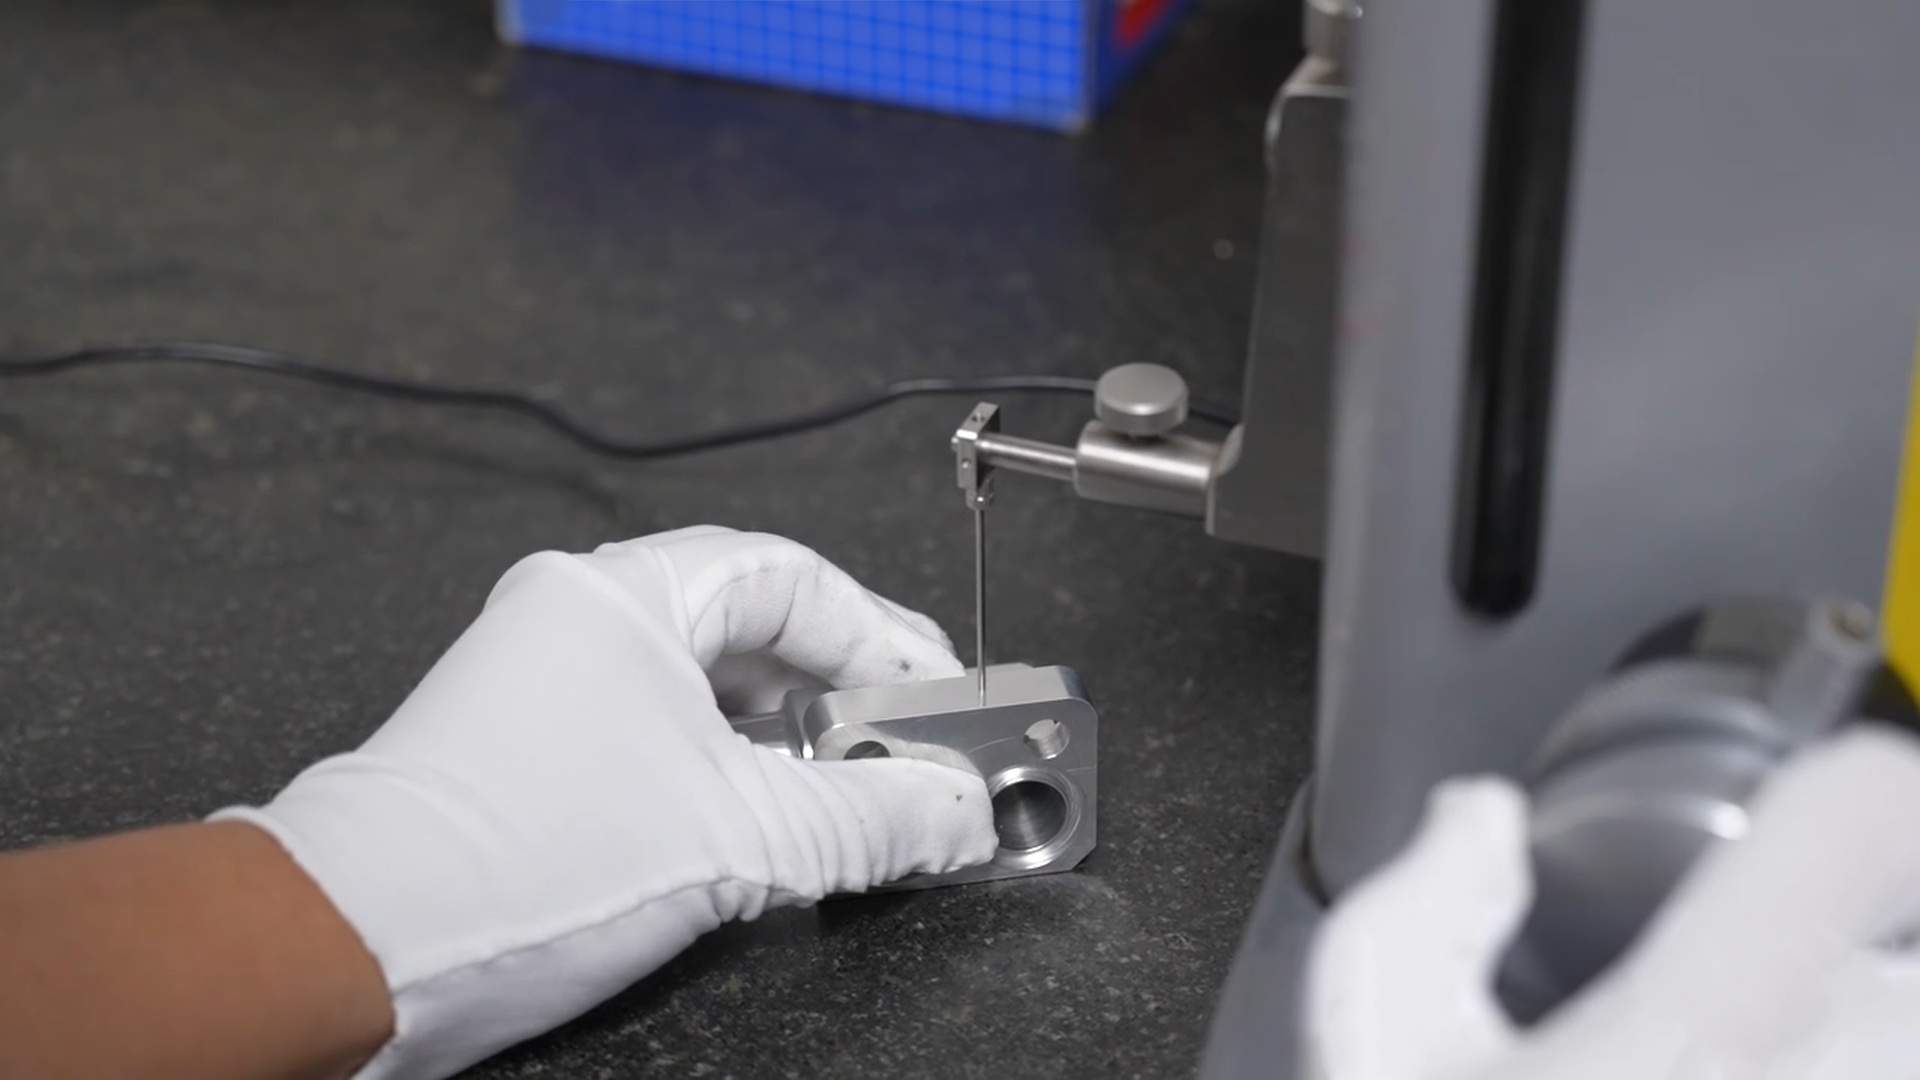
FROM PROTOTYPE TO PRODUCTION
Timing is planned after the drawing is frozen and the fixture, material, quantity, finish and inspection requirements are understood.
Typically 3–7 days after requirements are confirmed · Validate datum strategy, wall condition and critical features
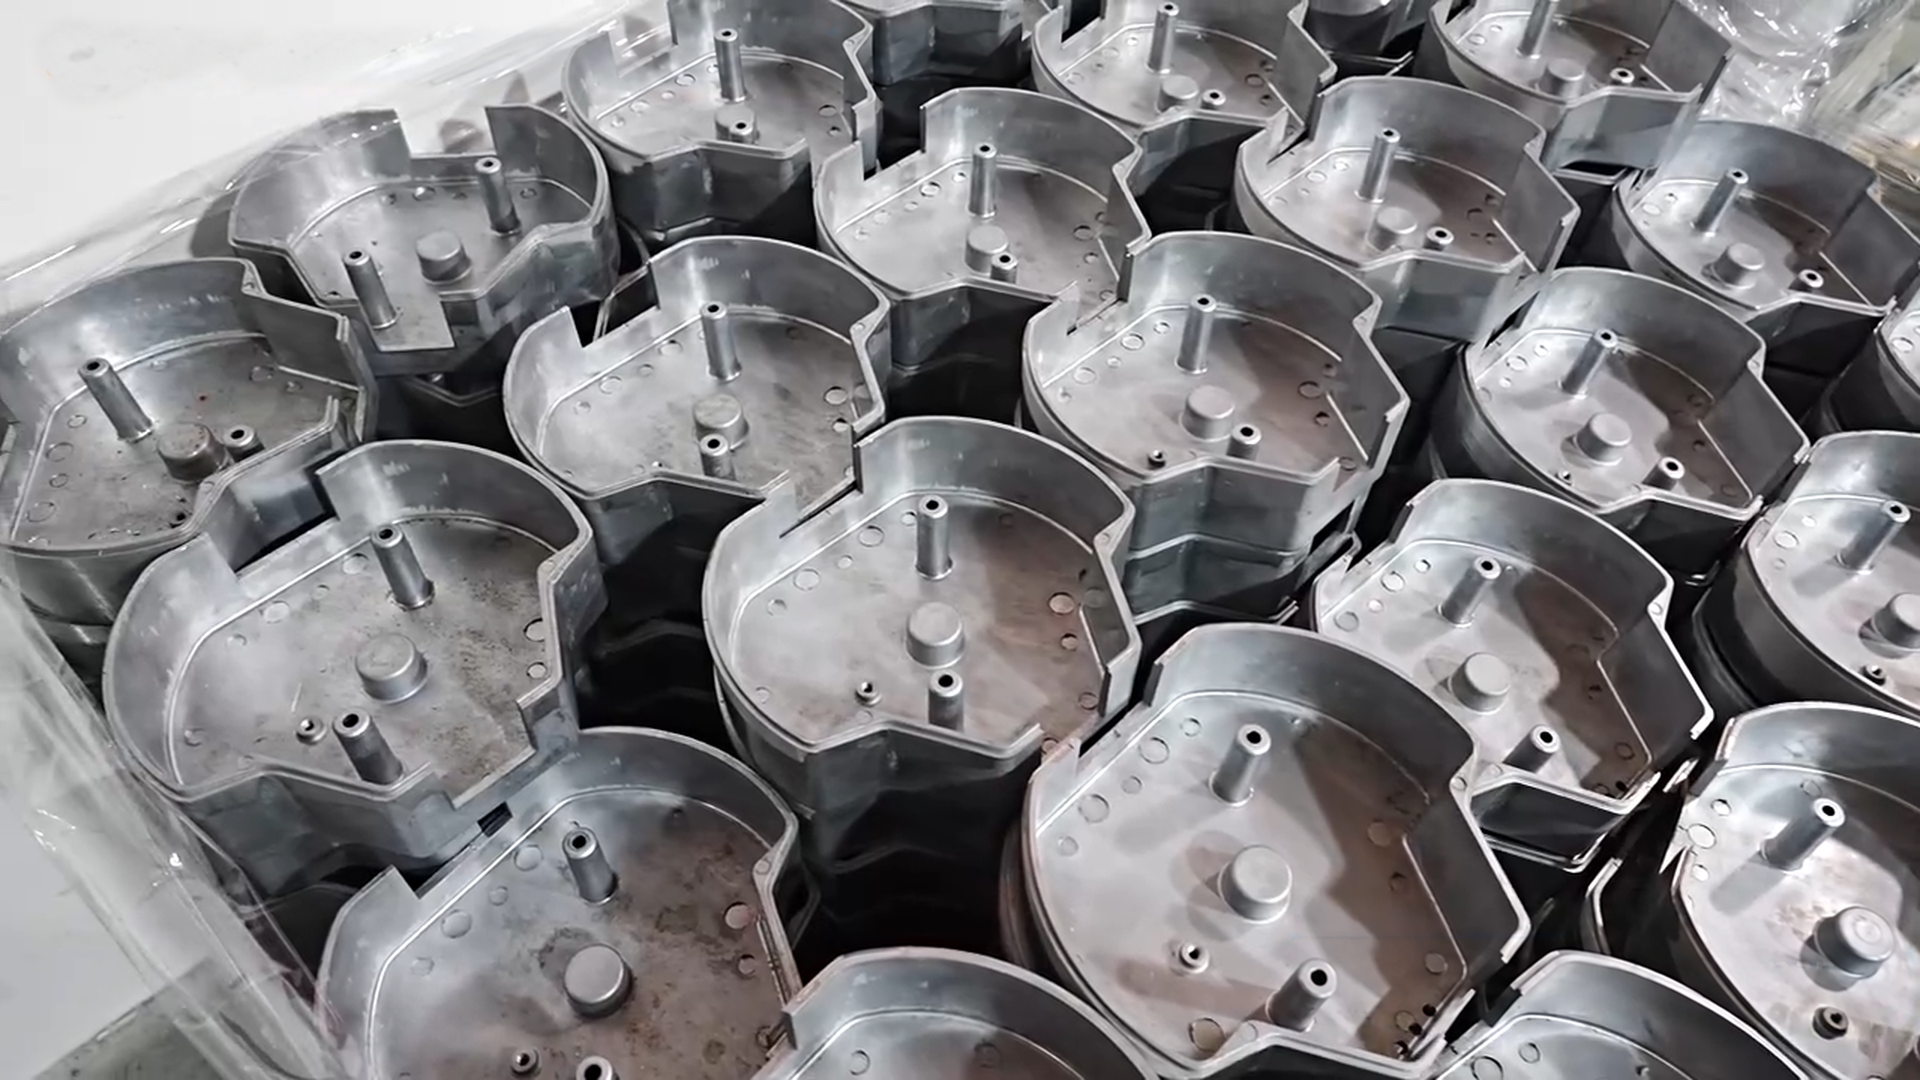
Plan fixture approach, material and finish before scheduling · Confirm inspection requirements
Typically 25 days after drawing freeze · Timing depends on part geometry, quantity, secondary operations and inspection scope
FREQUENTLY ASKED QUESTIONS